What the refresher session covers on site
The session is built around the day-to-day jobs crews actually face on HDPE pipe. We work through joint preparation, pipe end alignment, facing, heater plate use, changeover timing, fusion pressure, cooling time and bead inspection, with the machine settings matched to the pipe size and SDR in front of the team.
Training can be done on your machine or on equipment prepared for the visit. We cover the points that usually slip after a break from fusion work, including clamp grip, pipe end cleanliness, hydraulic pressure checks and the logs needed when weld records must be kept clear.
- Pipe size ranges from small bore lines to larger mine installations
- SDR matching and wall thickness checks before a weld starts
- Heating, timing and clean changeover between heat and fusion
- Bead appearance, squeeze out and basic visual acceptance
- Weld logging notes for job cards and site records
How the training is put together
Refreshers start from the work type, machine model and site pipe sizes. That lets us set the session around the actual joints your crew will make.
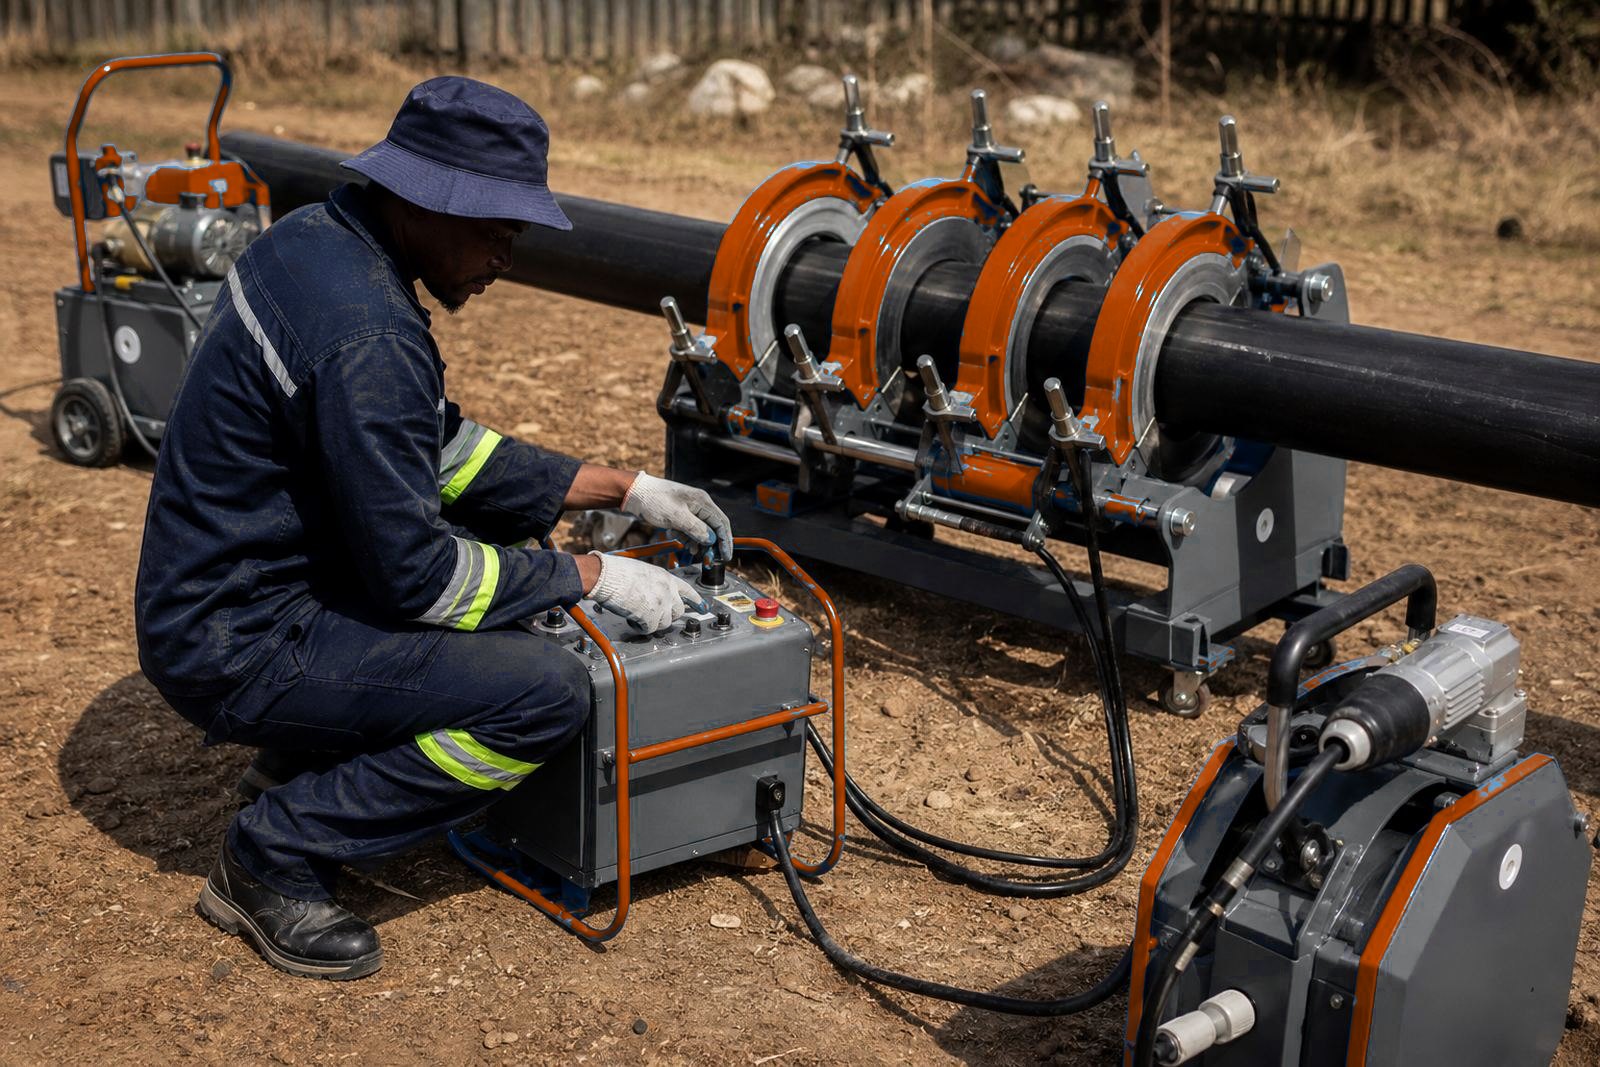
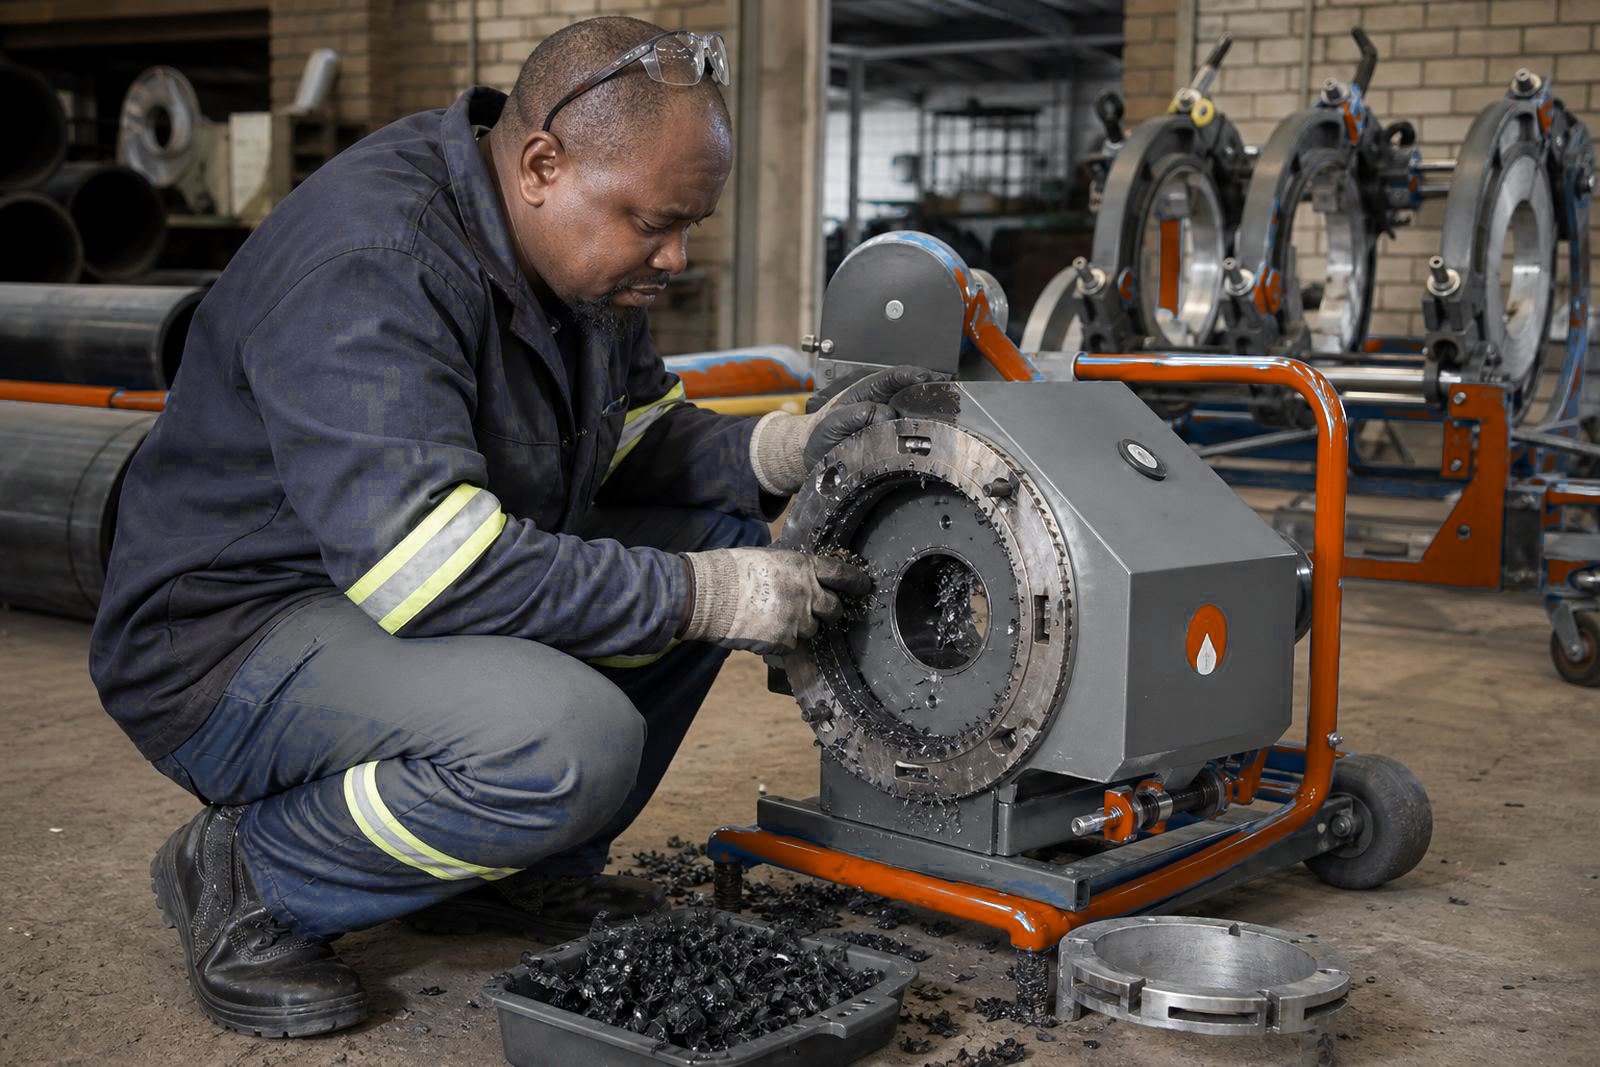
The refresher then moves in a practical sequence. First the team revisits machine setup and clamp alignment, then the facer and heater plate are checked, after that we step through one or more full weld cycles with close attention to pressure rise, changeover timing and cooling under load.
- Short briefing on the pipe, machine and work method in use
- Demonstration of setup, facing and alignment
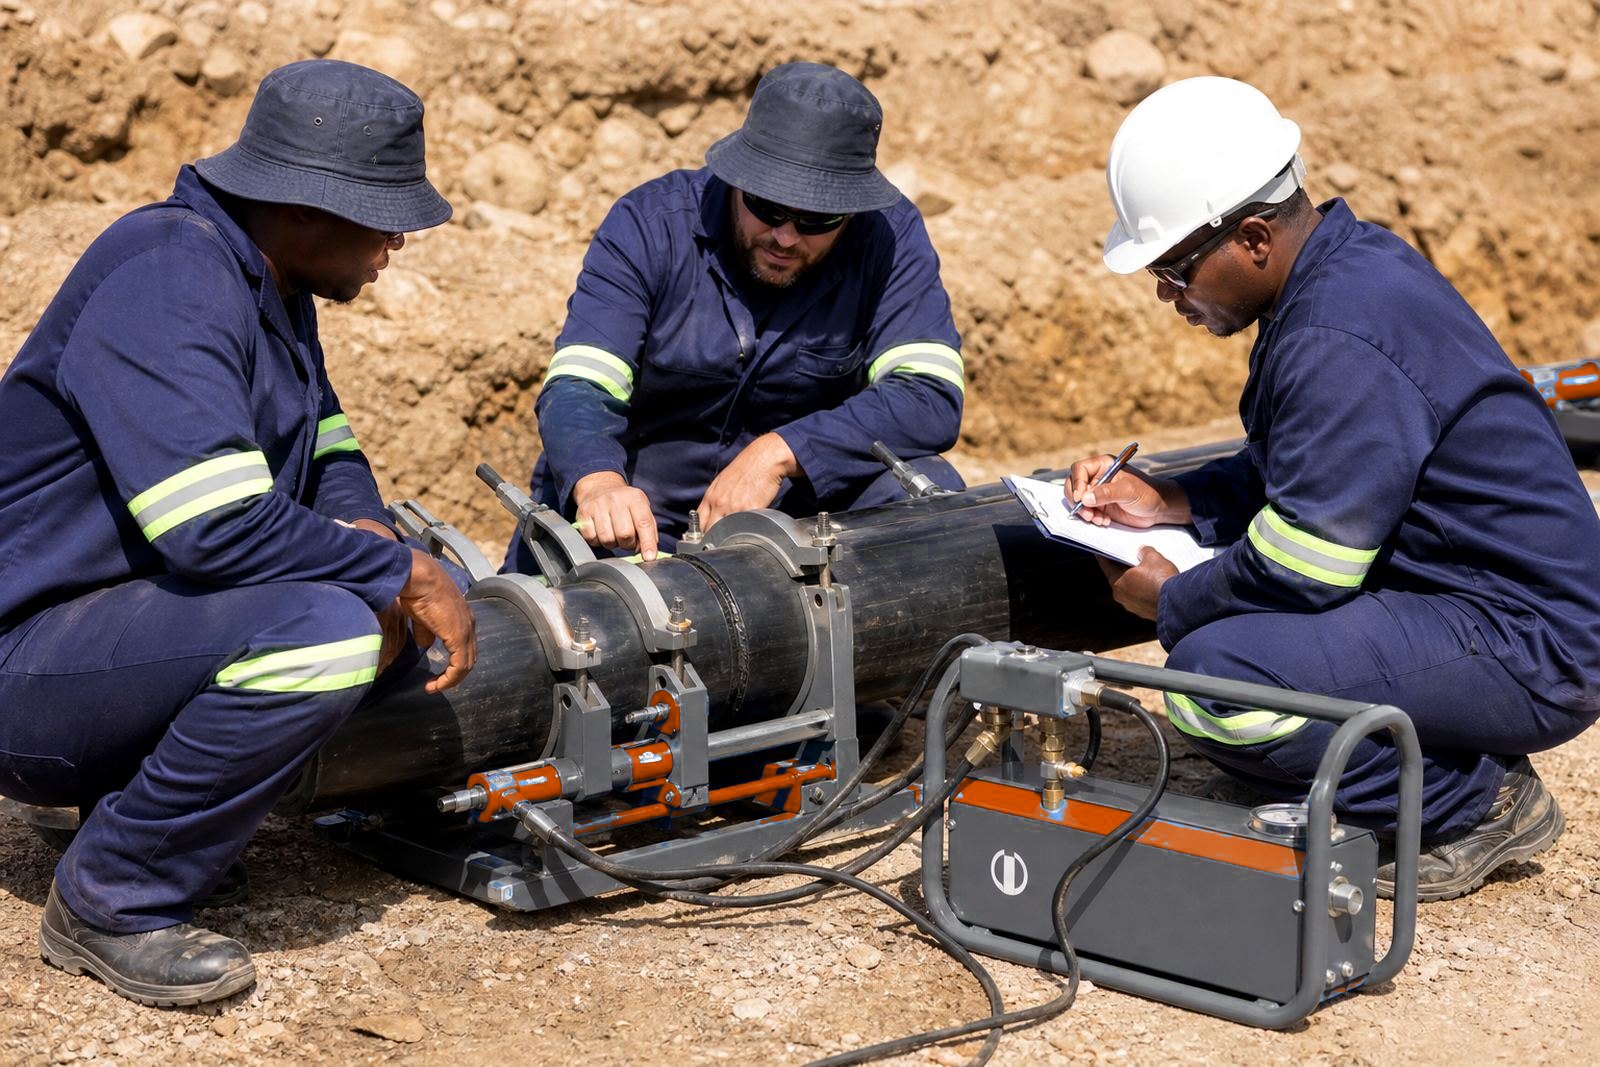
- Supervised weld sequence with corrections where needed
- Bead review and log sheet guidance at the end
When to book a refresher
Crews often ask for this after a gap in HDPE work, after staff changes, or when a job calls for tighter control on welding records. It suits machines shared by crews who have drifted into different methods.
Refresher training brings a changed crew back onto one method. Coastal humidity, dusty mining areas and cold early starts can all affect the way a joint is prepared, so the session is adjusted to the local conditions and the work sequence the team will face.
Training flow, from the first check to the joint record
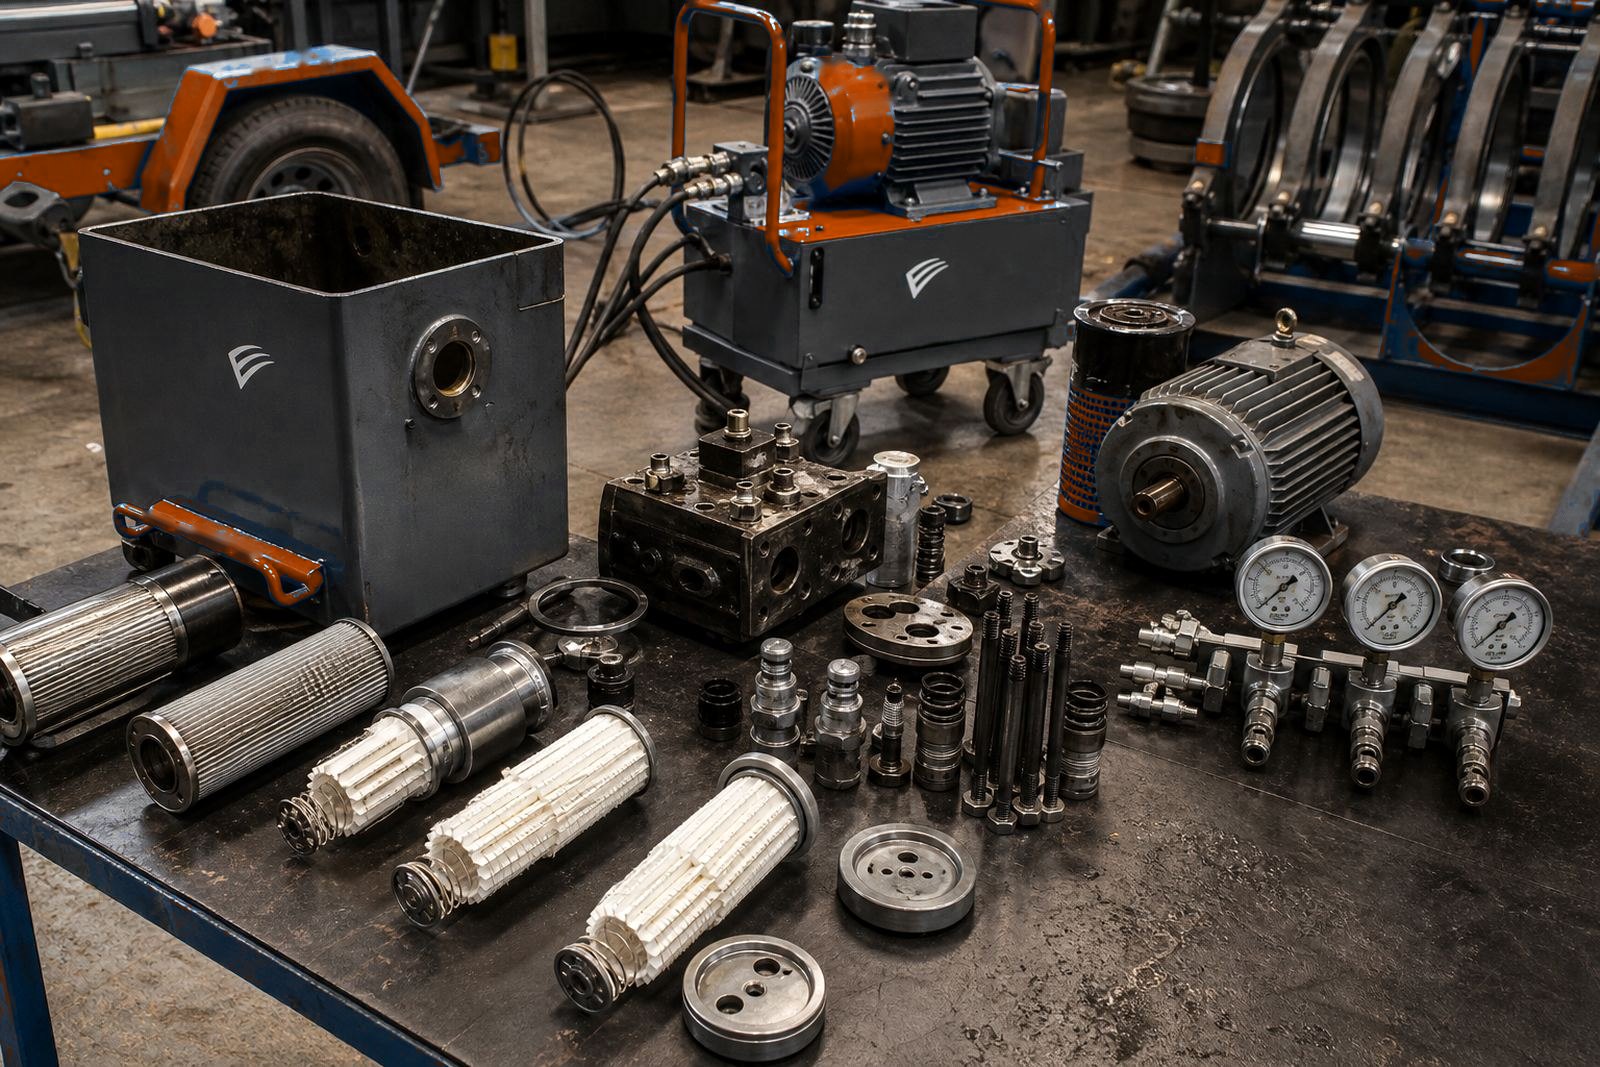
Every refresher is practical. We look at the machine, the facer, the heater plate, the clamps and the hydraulic system, then move into controlled welds. Where needed, we also cover how to spot plate contamination, uneven facing, poor alignment and cooling that was cut short.
Get the operators back into a steady rhythm so the weld sequence is repeatable and the record keeping makes sense to the people checking the job later.
- Machine and tool inspection before the first joint
- Pipe ends squared and cleaned before facing
- Fusion pressure applied and held for the right cooling period
- Weld bead reviewed for size, shape and consistency
Pricing approach and how the quote is built
Refresher pricing is based on the number of operators, location, machine type, whether the session is on your site or tied to a hire unit, and the amount of practical welding. A short crew refresher on one machine is priced differently from a wider session that covers several operators, multiple pipe sizes or extra logging help.
If heater plate checks are needed alongside the training, they are set out separately so the scope stays clear. Before the session starts, the crew knows what is included, which keeps things clear on site.
Aftercare for crews that want the method to hold
After the session, we can leave the team with a clear weld sequence and notes on the machine settings used during training. Where the site keeps logs, we can also help tidy the format so future joints are easier to record and review.
Servicing needs such as uneven facer cuts or drifting clamps are passed to our servicing team. This leaves the crew able to continue with a cleaner process on the next job and in their ongoing work.
Who the refresher suits
The refresher also suits projects with several pipe sizes, changes in SDR, or operators who need a reset before work starts on an active programme.
The training can also be arranged for Mpumalanga sites and Northern Cape work where crews need practical help on the ground.
Key facts
| Service | Refresher Training |
|---|---|
| Equipment scope | Butt-fusion HDPE pipe welding machines, facing tools, heater plates and clamps |
| Core topics | Facing, heating, changeover, fusion pressure, cooling time and bead inspection |
| Pipe range | Small bore lines through to larger mining pipe sizes, subject to machine capacity |
| Records support | Weld logging help and site documentation guidance |
| Area covered |