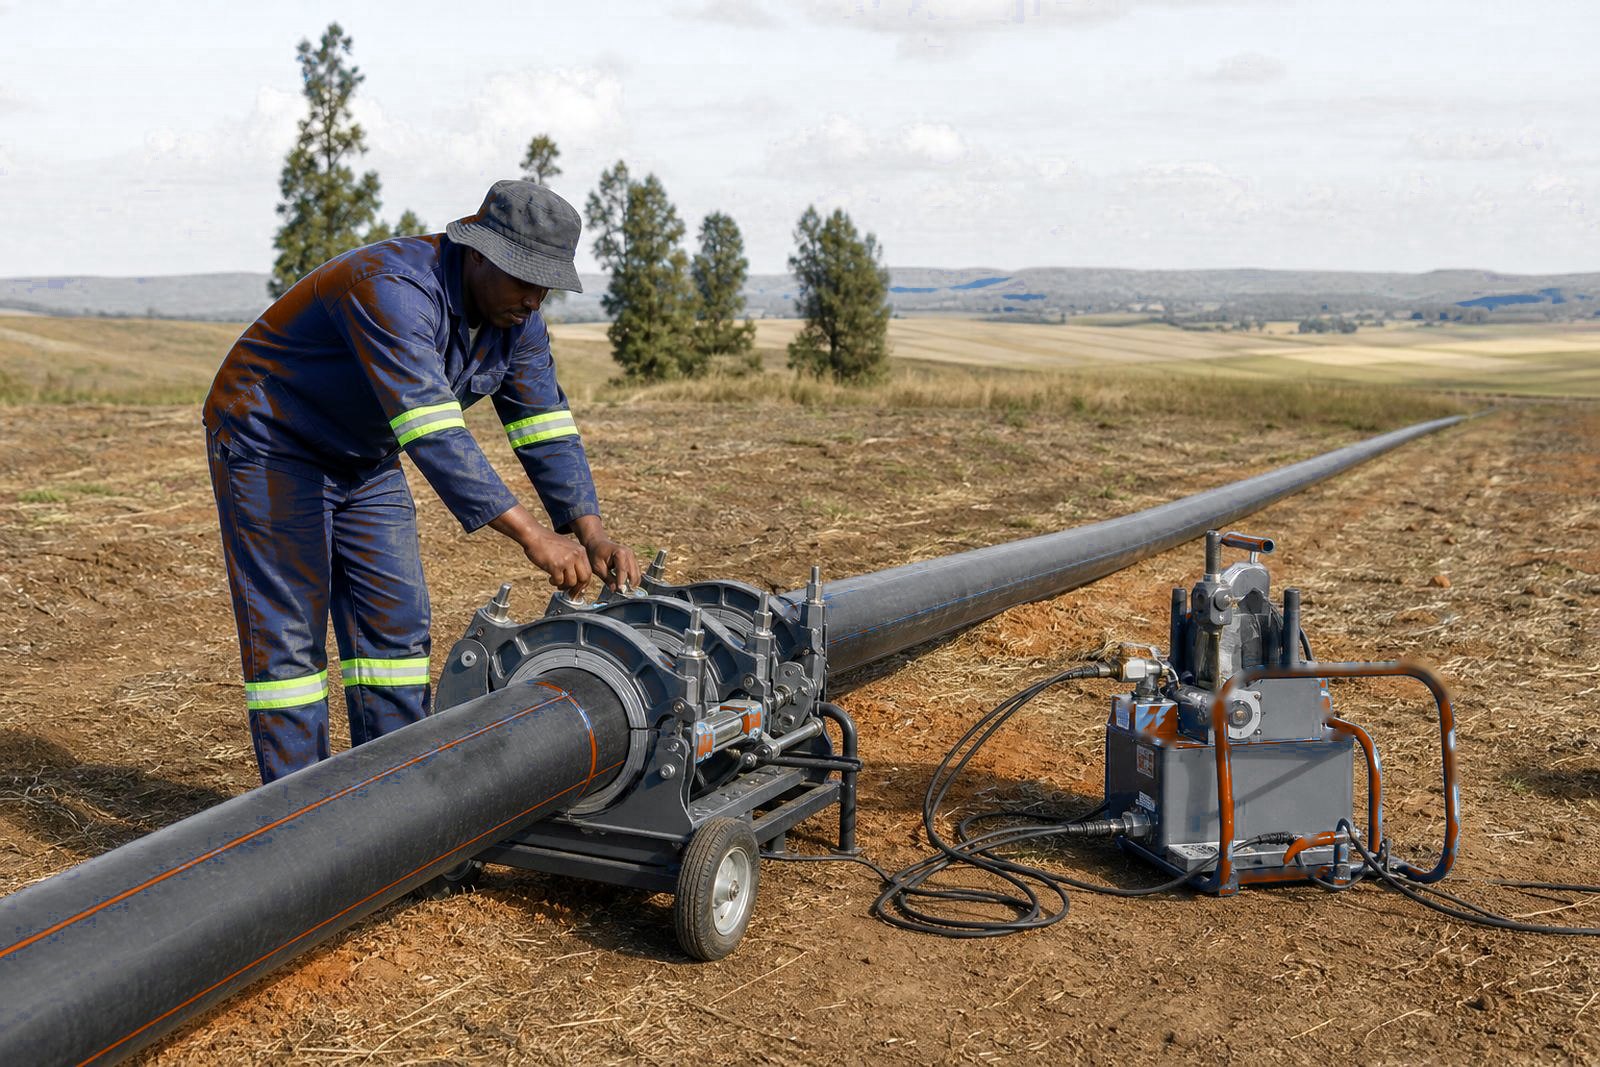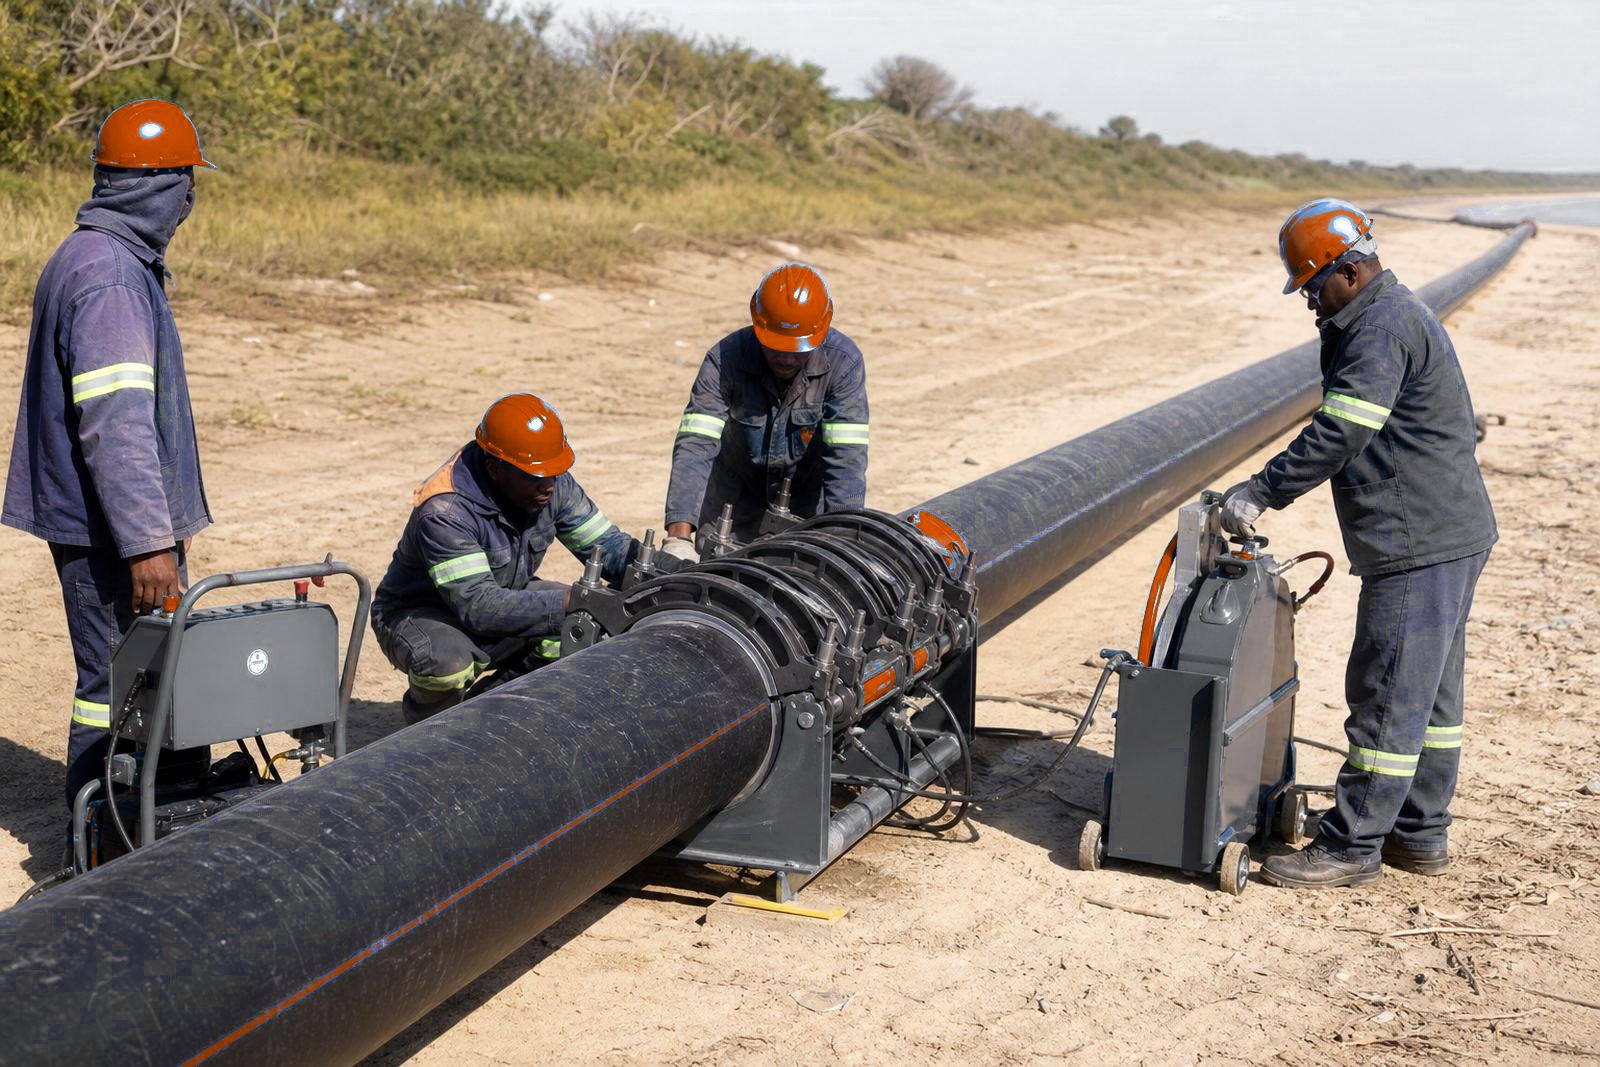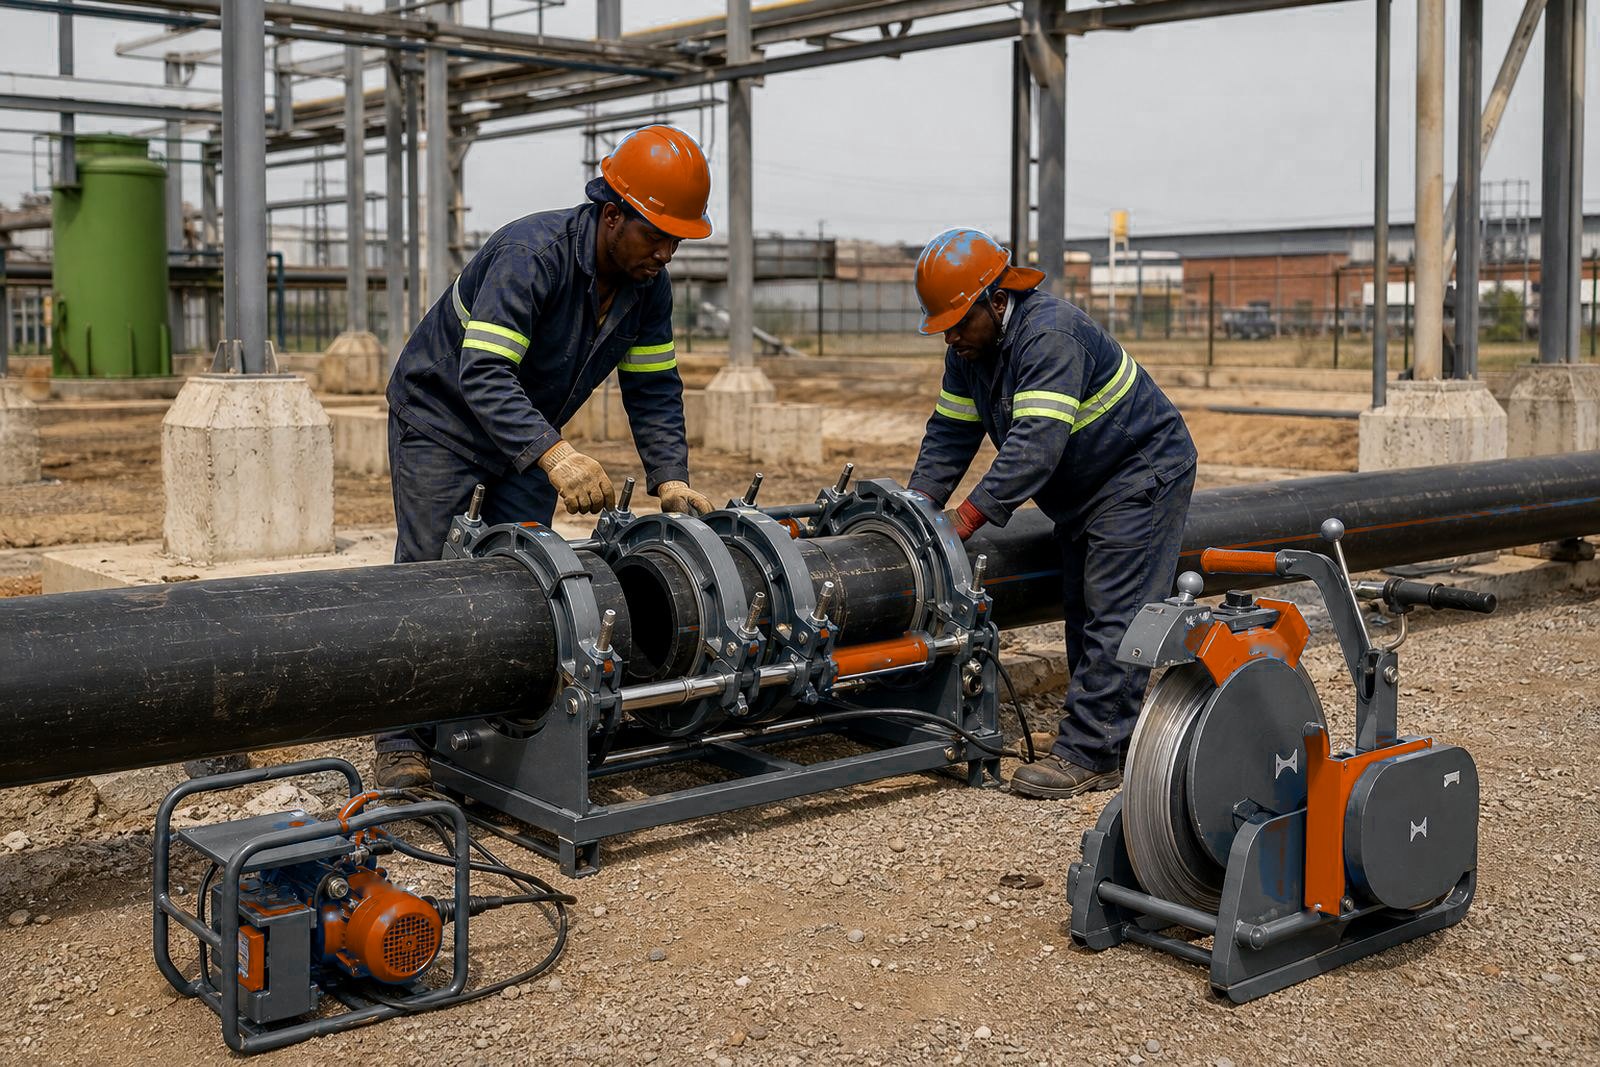
Plant conditions in Boksburg set the brief
Before any fusion started, the pipe ends were squared, cleaned and faced so the hot plate could meet fresh material on the pipe end. A poor face gives a weak bead or an uneven joint.
For Boksburg we supplied machine, facer, plate and clamps, then coached operators through the full sequence. The settings were matched to the pipe diameter and SDR on each run, and the crew kept the pipe ends stable during changeover so the bead formed evenly around the circumference.
- Facing and alignment on each joint
- Heat soak and changeover control
- Bead inspection after each weld
Workshop prep before the site shift
The first stage ran in the workshop, where the machine was checked, the heater plate condition was verified and the clamps were aligned for the pipe dimensions involved. That cut down on surprises once the team moved onto the plant floor, where space was tighter and the shutdown clock was fixed.
We also helped the crew set up a weld log so each joint could be tied back to its pipe size, SDR and operator. Maintenance teams use that record to compare sections or trace a joint after commissioning.
- Machine check and functional setup
- Heater plate condition review
- Clamp alignment for the pipe range on site
- Weld logging help for handover records
Training tied to the upgrade
Operator training was built around the actual joints the crew had to make in the trade. We covered pipe end preparation, heater plate contact, timing, pressure build-up and the cooling period before release, because those steps affect the finished weld.
Boksburg operators learned to spot a thin bead, smeared face or uneven squeeze-out before the next joint. The setup was corrected before production welding began on the live plant.
- Operator training on the fusion sequence
- Bead inspection and visual checks
- Pressure control during cooling
- Refresher guidance for the site crew
Hire gear for the shutdown window
The job was done in a measured window over several weeks, with hired equipment rotated into place where needed. That kept the project moving even when the crew had to break work into smaller sections around plant access and isolation rules.
Our field technician handled practical checks on the machine, while the service side dealt with hydraulic pressure testing. Clamp alignment was checked before each new section, because even a slight shift can throw off the joint face and the fusion pressure on larger pipe.
- Machine hire for the shutdown period
- Field checks on equipment and accessories
What the Boksburg line needed at handover
The replacement line ended with a steady welding rhythm and a team that no longer stopped to reset basics. The weld logs were in place, the bead quality was more consistent and the pipe sections matched the planned SDR and diameter range for the job.
If we were standing off on a similar project again, we would keep the same order: workshop prep first, then machine setup, then a short run of supervised joints before the full site push. Crew stays steady and the plant team gets a clearer handover when the shutdown ends.
- Consistent fusion sequence across the joint run
- Documented welds for the replacement line
- Cleaner handover for plant maintenance teams
Key facts
| Project | Boksburg Plant Upgrade |
|---|---|
| Client type | Industrial plant maintenance team |
| Town | Boksburg |
| Pipe system | HDPE replacement lines |
| Service mix | Workshop prep, site welding and hire |
| Equipment range | Butt-fusion machine, facer, heater plate, clamps |