A clearer panel for the fusion operator
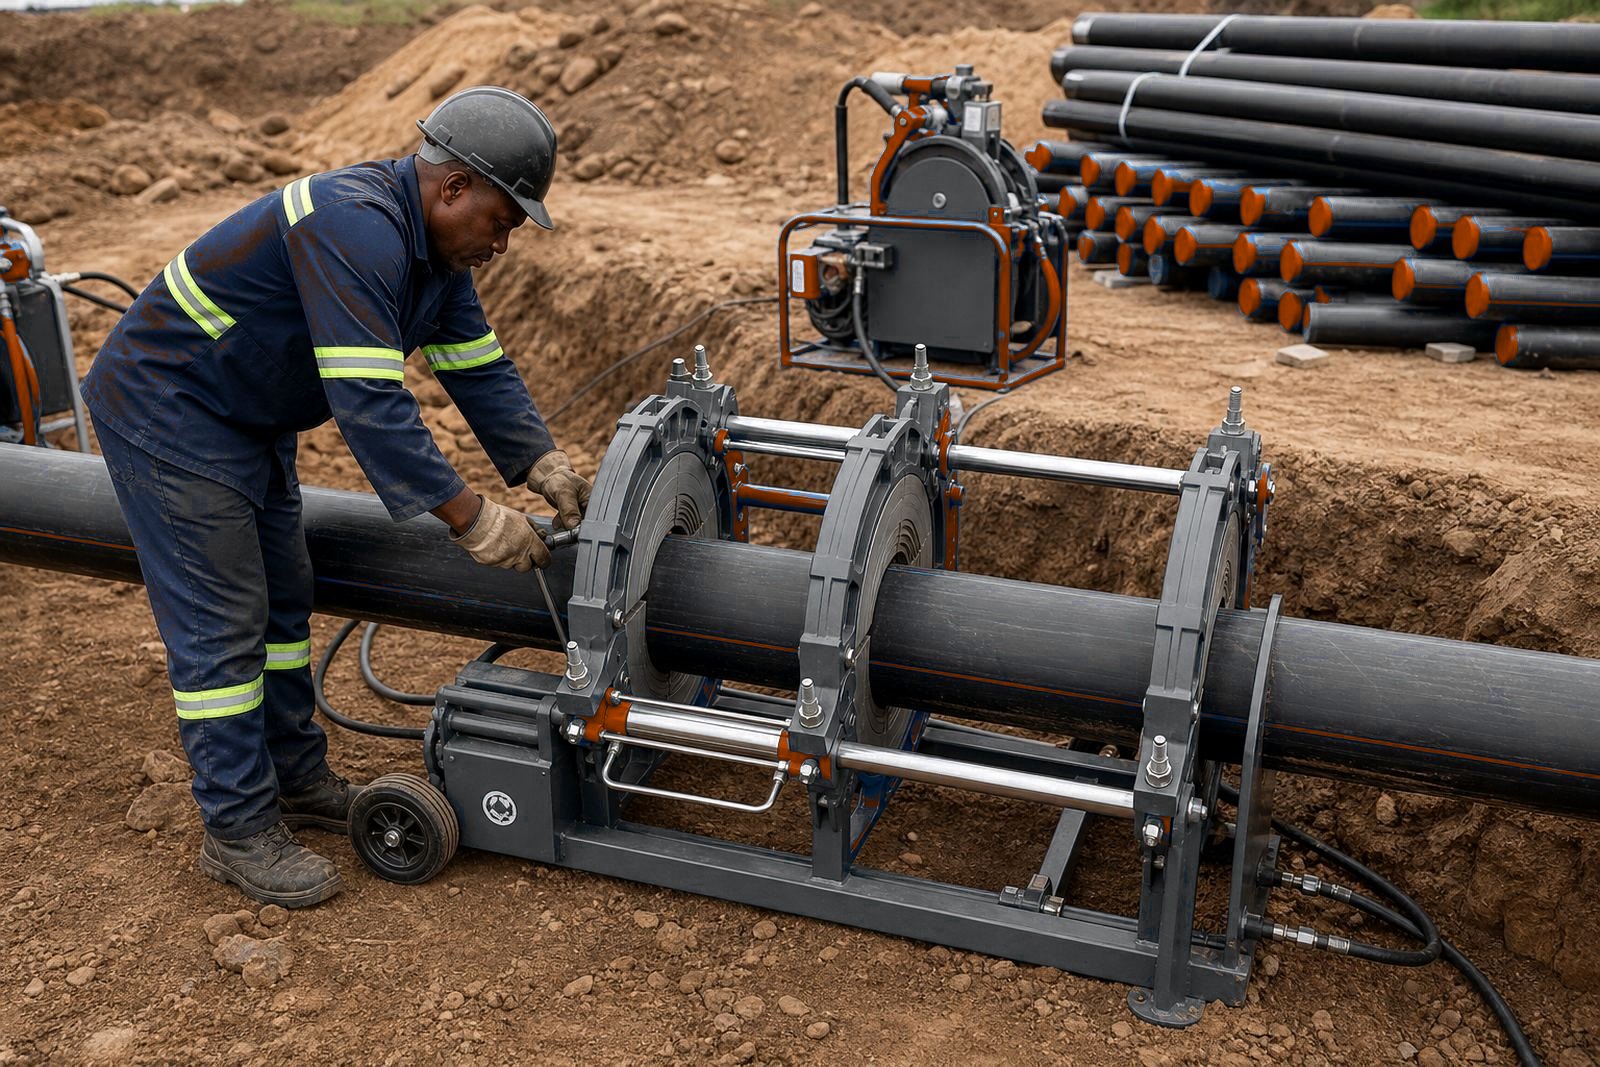
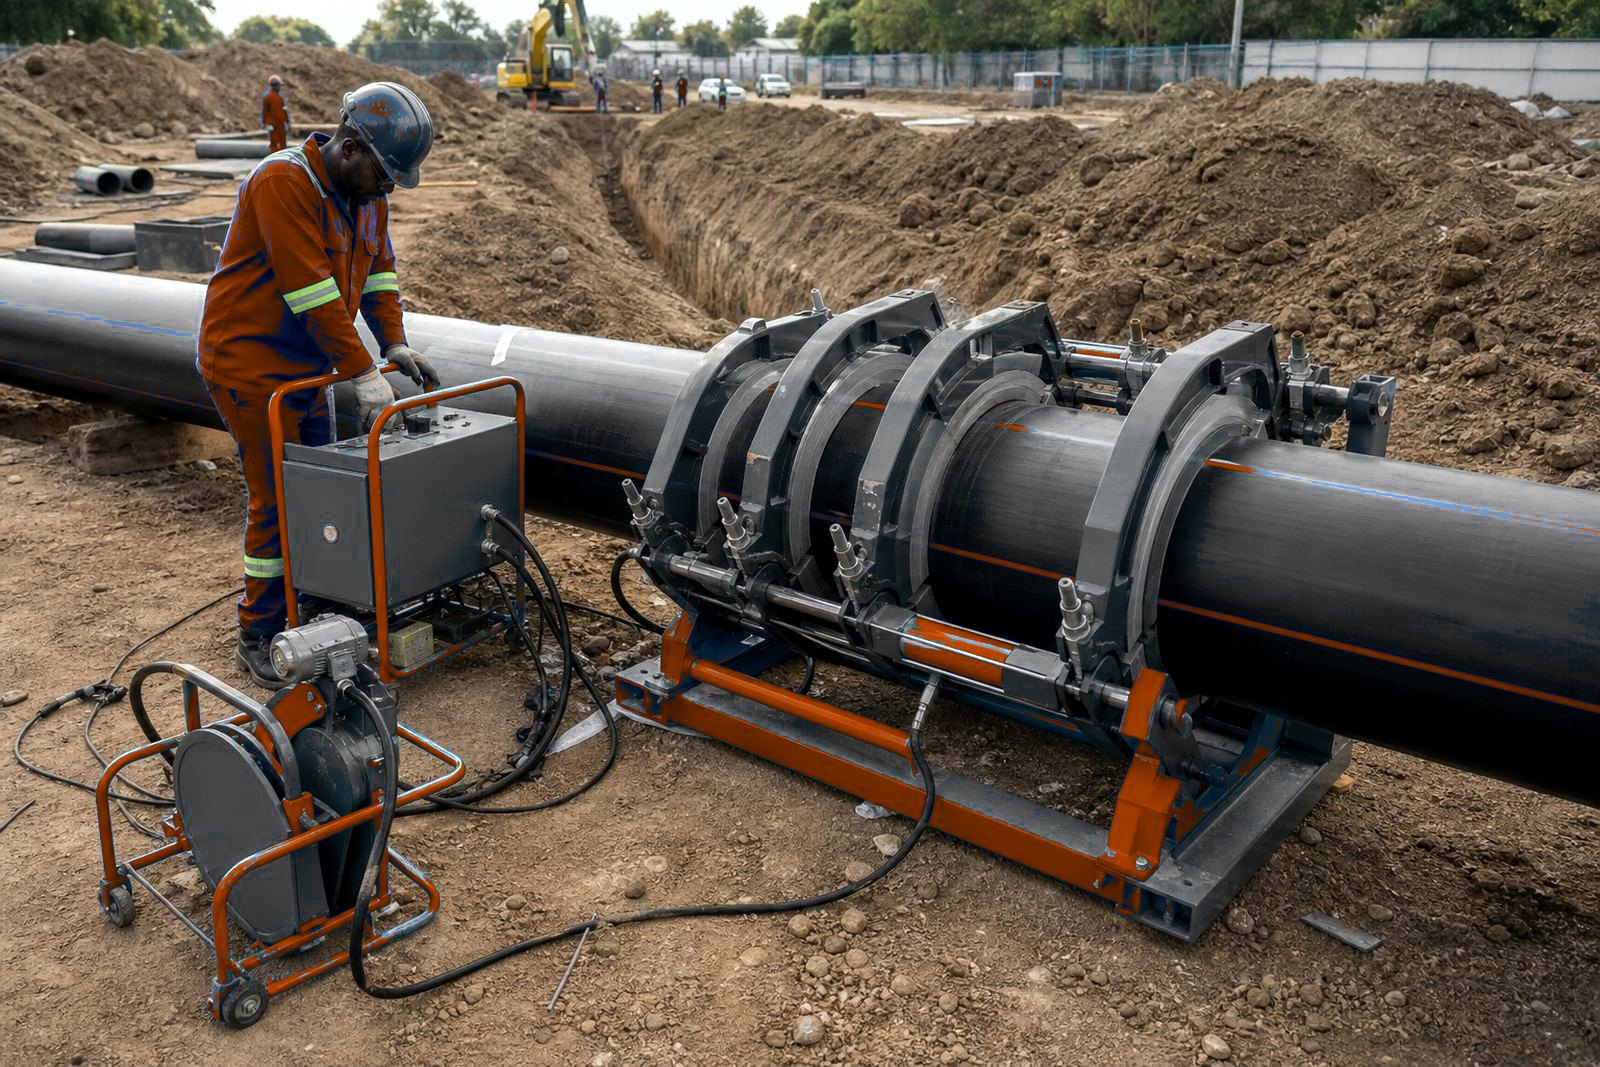
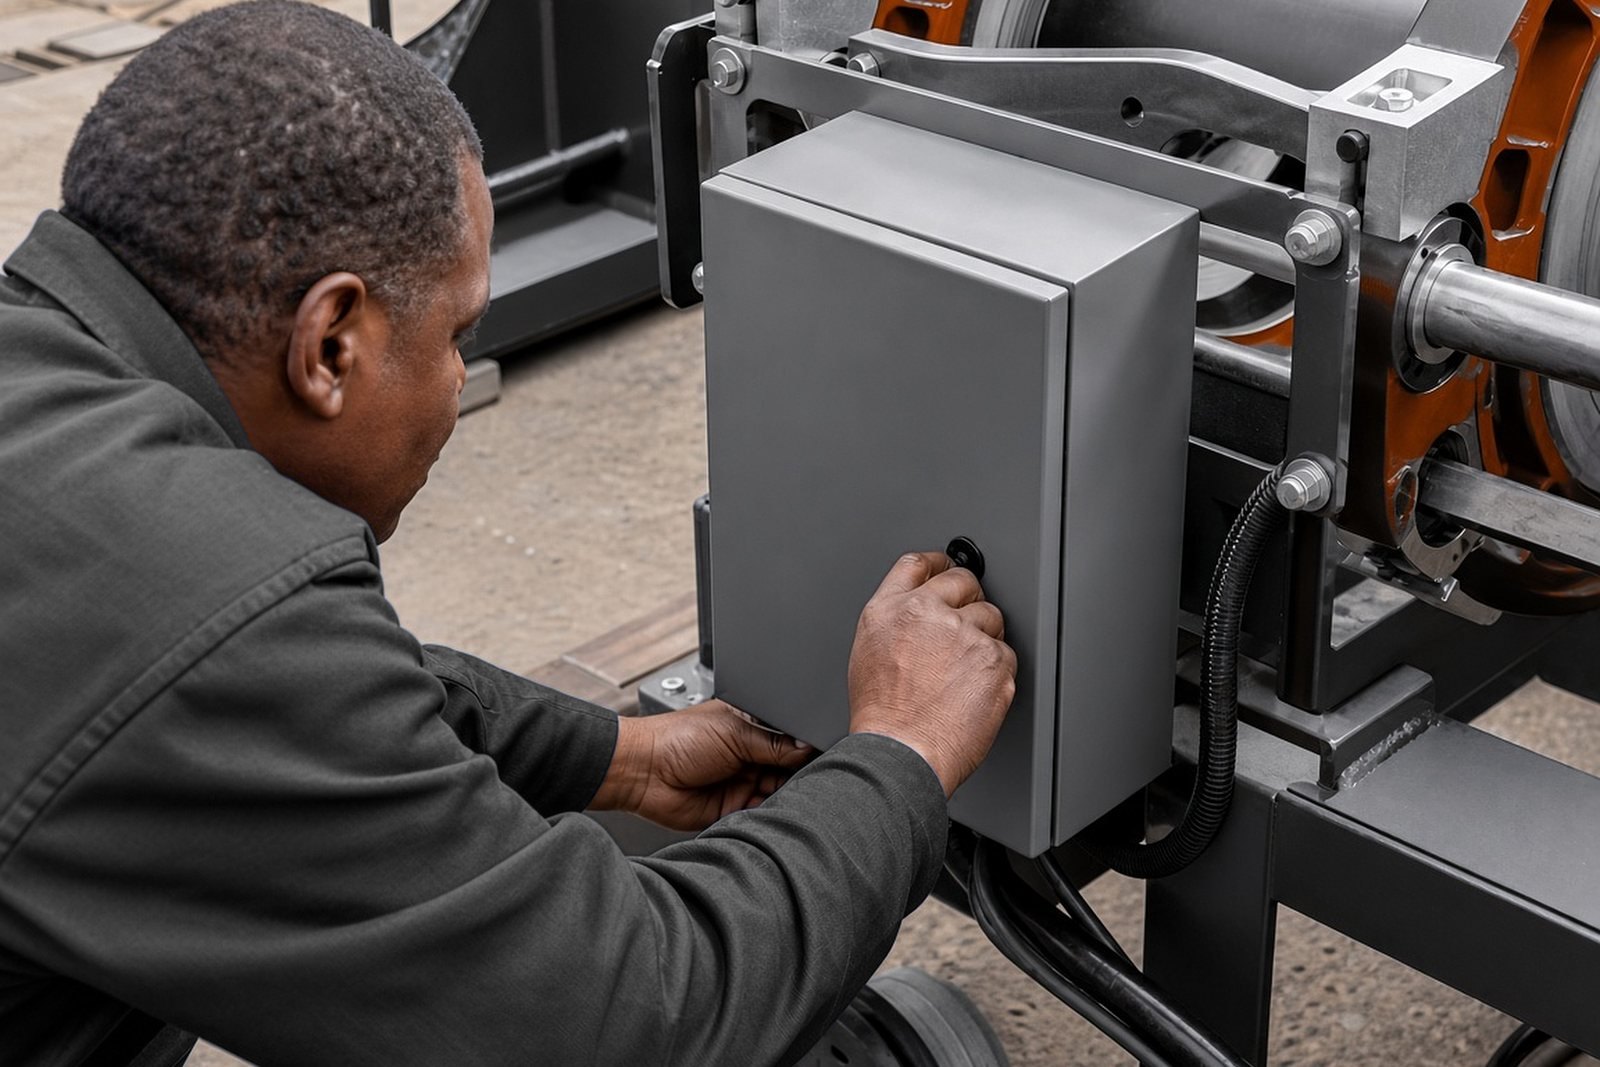
This control box is fitted to butt-fusion machines used on HDPE pipe joints and controls temperature, pressure and timing on every cycle. The upgraded layout gives the operator a cleaner display for heater plate temperature, fusion pressure and changeover timing, so the sequence is easier to follow during long runs on site.
It is used on welding sets that handle common HDPE pipe sizes and SDR ranges. The box guides the operator through facing, heating, changeover, fusion pressure and cooling time, and shows each reading against the set value.
- Clearer heater plate temperature display
- Pressure indication during fusion and hold phases
- Record support for weld logs where required
Sizes and control options for different welders
The upgrade is supplied to suit different machine frames and control layouts, because butt-fusion rigs do not all use the same panel cut-out or wiring arrangement. On some machines the control box is a direct replacement for an older unit, while on others it is supplied with matched sensors, pressure transducers and loom changes to suit the hydraulic system.
For crews handling pipe from smaller service work through to larger mainline joints, the display format and input range need to match the machine’s working band. The match covers the heater plate range, the hydraulic pressure window and the joint size the frame is built to carry.
- Single display or dual display options, depending on the machine
- Matching probe, sensor and transducer inputs
- Set-up for manual monitoring or logged cycle use
- Housing and connectors matched to the frame layout
Machines that suit the control box upgrade
Weld records, shared machines and a foreman who reads the cycle from a distance all favour the upgraded box.
On jobs where pipe diameter changes through the week, from smaller runs into larger bore sections, the operator can follow the set pressure and heating time with more confidence. On exposed sites, the control box needs to stay readable in dust, humidity and glare.
- Water pipeline installation and repair
- Workshop welding and field welding crews
Fitting, wiring and pressure checks
Fitting the upgrade calls for proper electrical and hydraulic checking, with the wiring matched to the machine’s supply, signal paths and emergency controls, and the pressure reading agreed.
When the control box is installed, the operator should test the heater reading against a known reference and check that fusion pressure rises and holds as expected. Clock, cycle settings and memory are tested under normal welding conditions before an upgraded unit leaves the workshop.
- Confirm machine model and frame size
- Check supply voltage and internal wiring layout
- Match pressure sensor type and range
- Test display, alarms and logging after fitting
Care between weld runs
A control box lasts better when it is kept dry, clean and free of grit from the pipe prep area. Dust from cutting and facing can work into buttons, plugs and terminals, and that is a nuisance when a crew is trying to keep a fusion sequence steady.
On outdoor jobs, cover the panel when the machine is parked and inspect cable ends for wear, bent pins and loose connectors. If the display starts drifting or the pressure reading looks uneven, the machine should be checked before it goes back into the line-up and another joint is made.
- After use, give the panel a dry wipe with a cloth
- Keep connectors free of mud and metal swarf
- Inspect cables for cuts, crushed sections and loosened plugs
- Schedule periodic calibration checks with servicing
Details to confirm before ordering
Control box orders need the machine make, frame size, supply voltage and pressure logging needs. Check the panel opening, connector style and sensor arrangement too, because a control box that looks similar can still be wrong for the hydraulic setup.
Pipe range and work type help too, from small service welding to heavy trench work. Mixed operator groups may need different display and cycle prompts, so tell us early.
- Machine model and frame type
- Voltage and wiring arrangement
- Required display functions and logging needs
Key facts
| Product type | Control box upgrade for HDPE butt-fusion welding machines |
|---|---|
| Display functions | Heater plate temperature, fusion pressure and cycle timing |
| Compatibility | Selected butt-fusion machine frames and hydraulic layouts |
| Logging | Optional weld cycle logging support, where the machine allows it |
| Typical use | Upgrading control on existing welding sets |
| Service support | Fitting, testing and operator training available |