Built for controlled butt-fusion on mid-range HDPE pipe
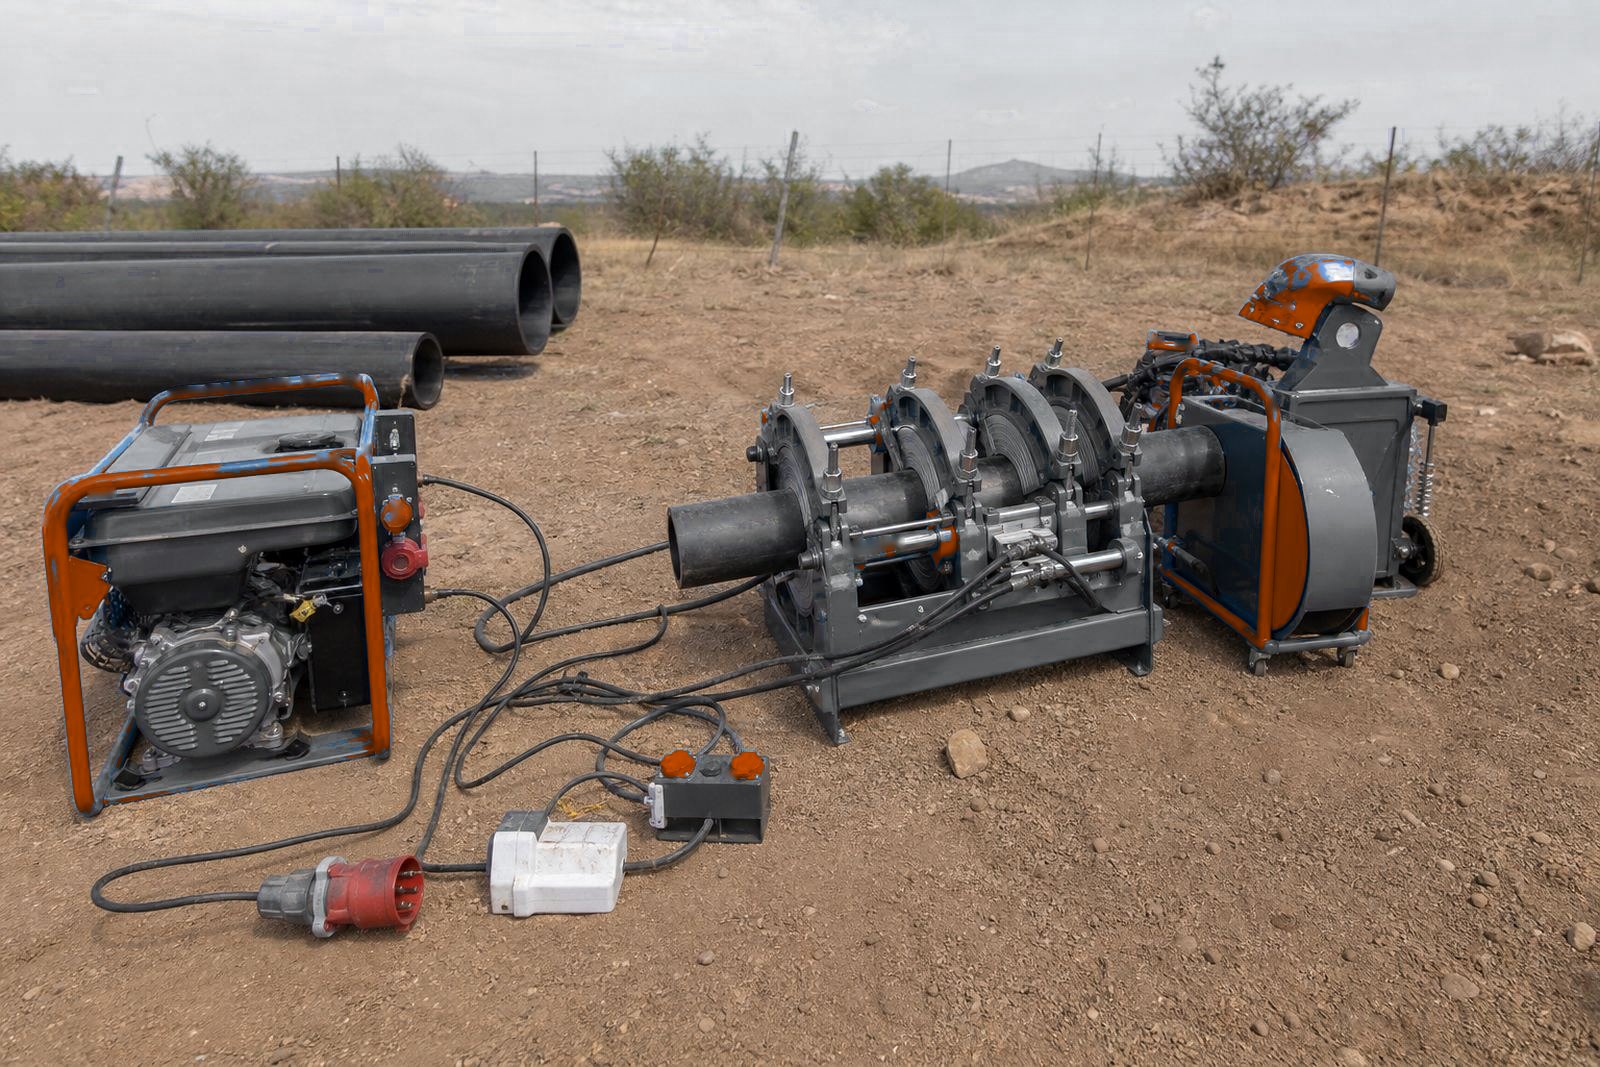
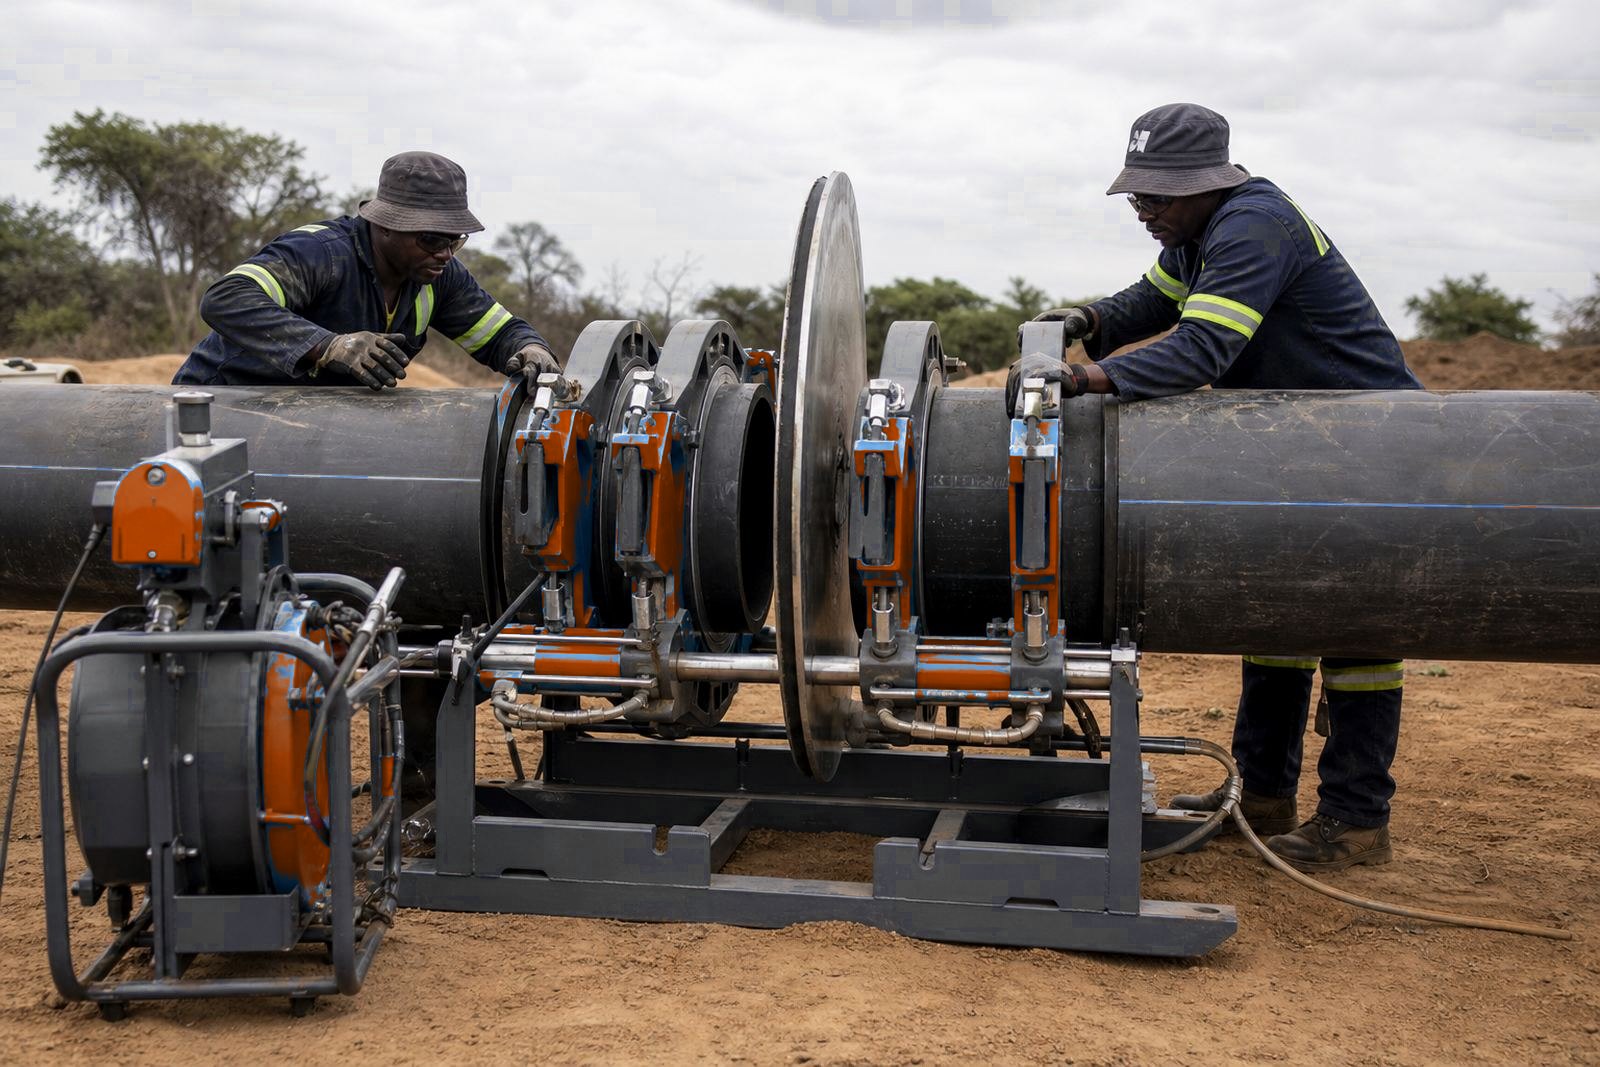
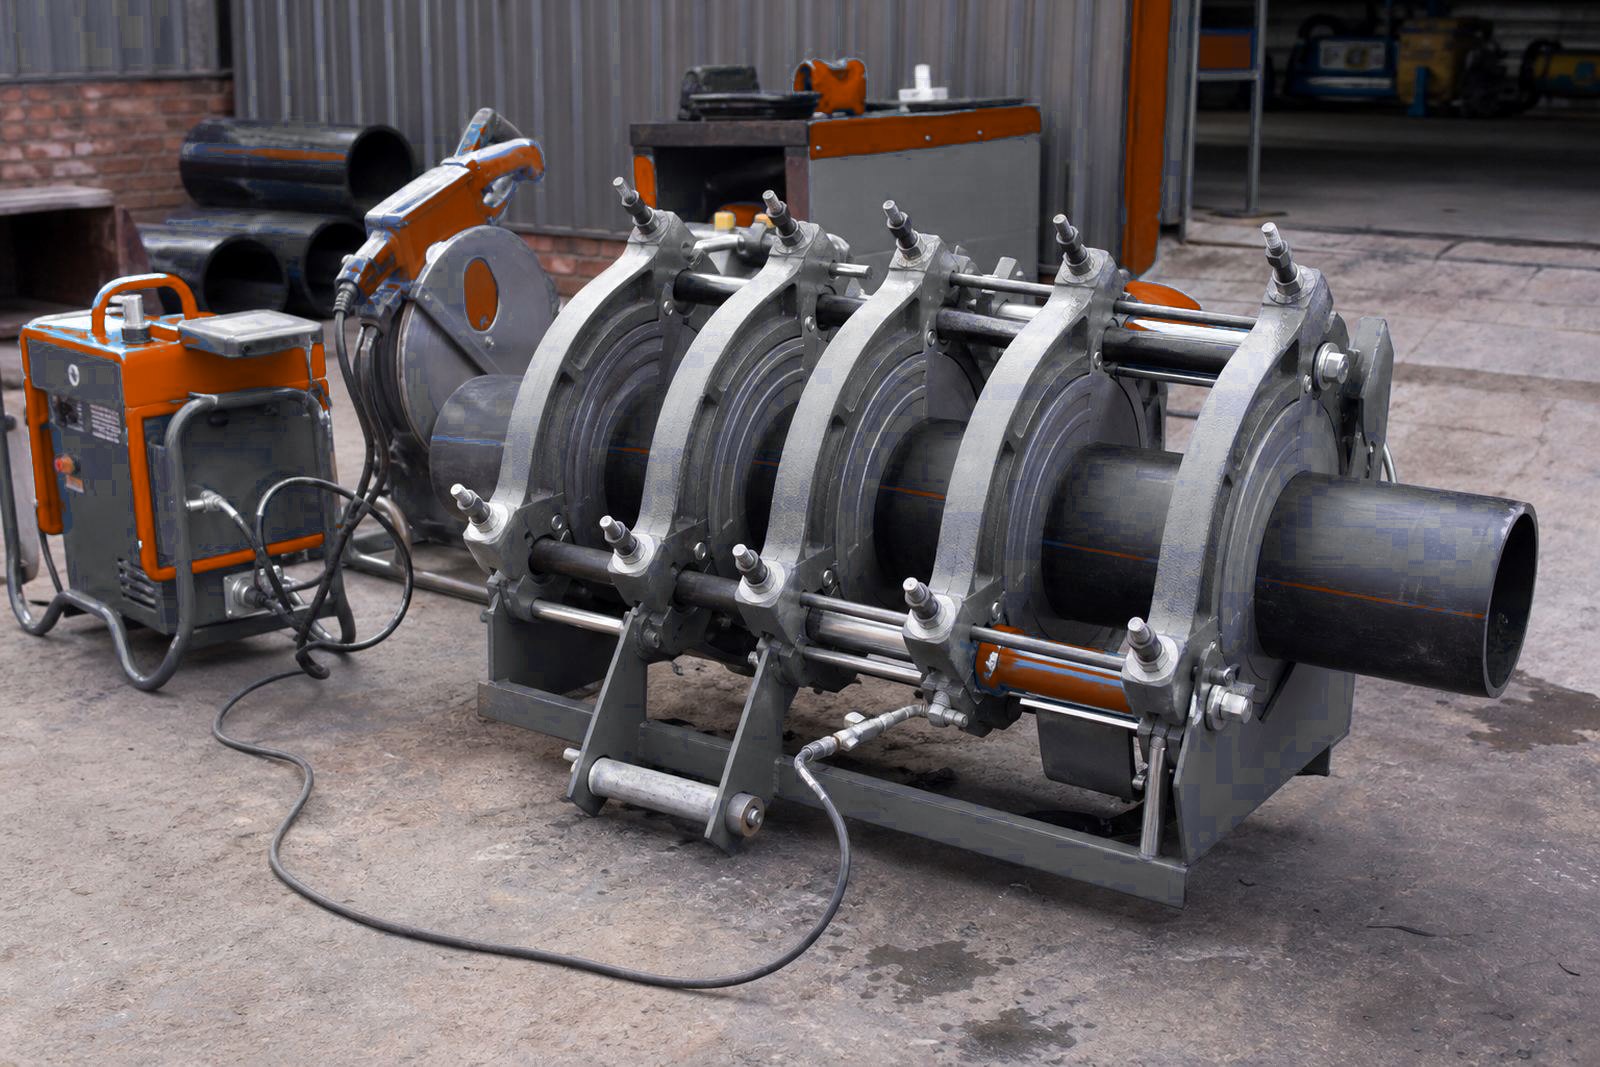
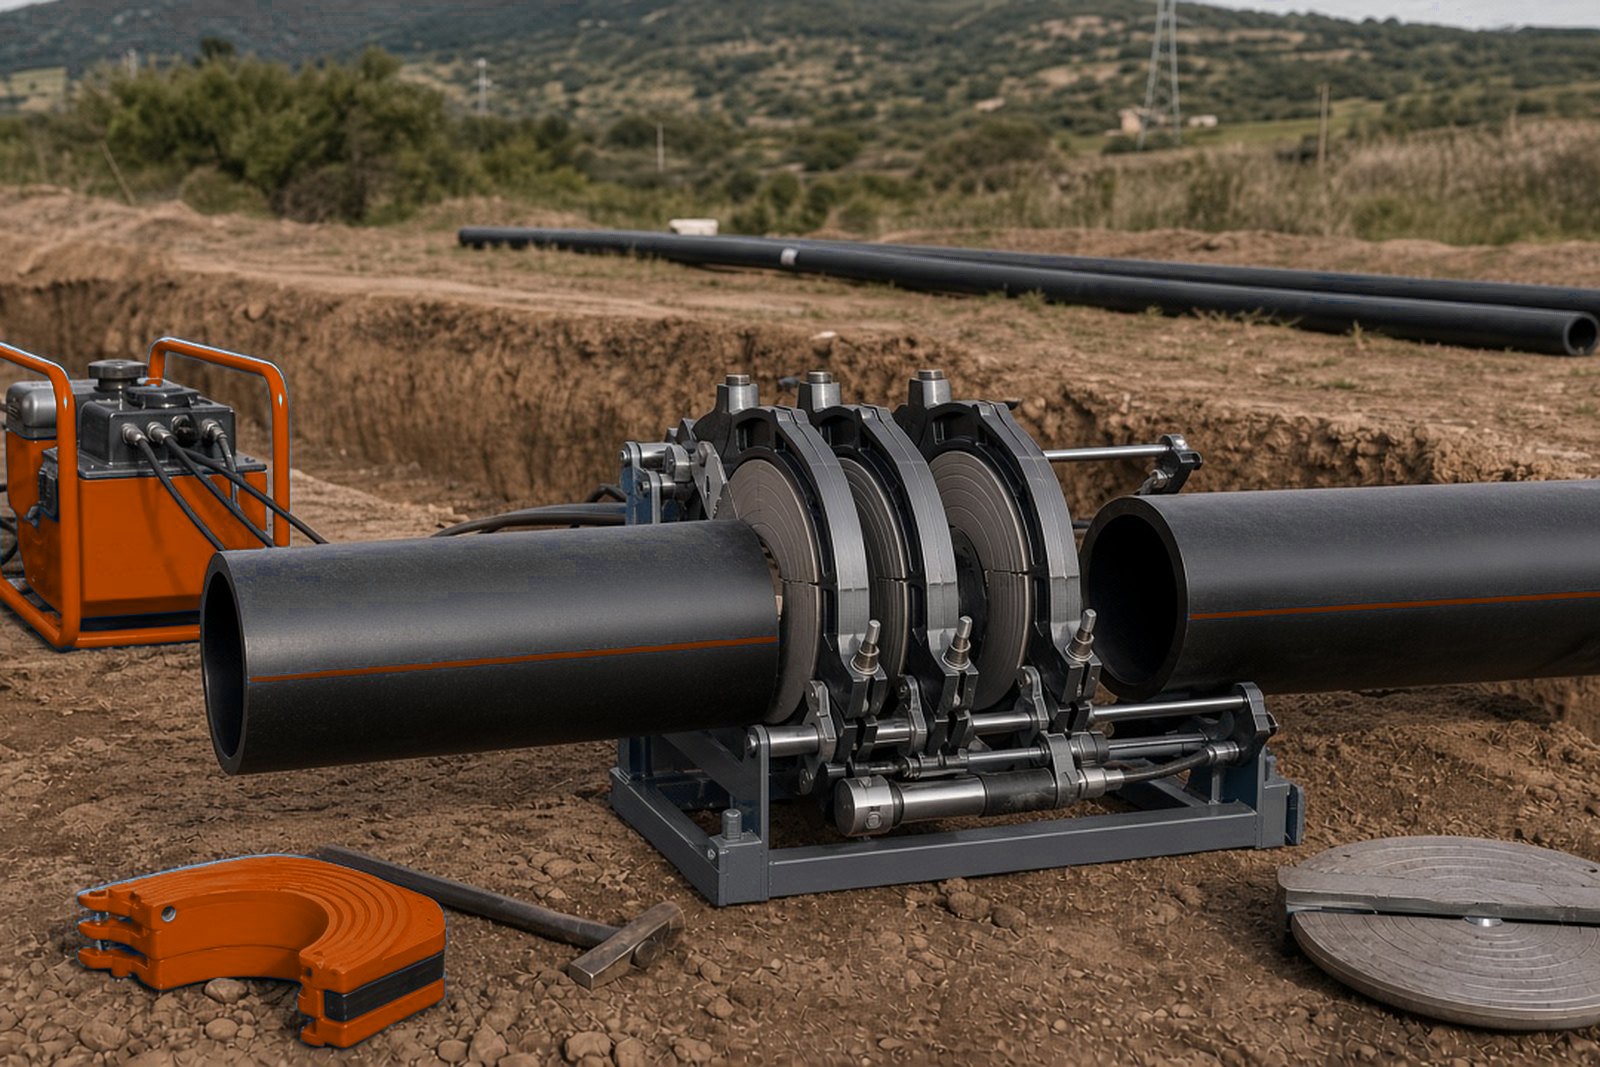
This hydraulic welder is set up for butt-fusion work on HDPE pipe from 160mm through to 355mm, with clamping and pressure control suited to field joints and yard work. We use it where the joint needs even facing, clean heater contact and steady fusion pressure through the cooling stage, with a fixed setup.
The chassis, jaws and pressure system are set up to keep everything in line while the operator works through preparation, bead build-up and cooling time. Water reticulation needs careful control when pipe wall, SDR and ambient conditions all need attention.
- Hydraulic clamping for stable pipe hold and alignment
- Suited to 160mm, 180mm, 200mm, 225mm, 250mm, 280mm, 315mm and 355mm pipe sizes
- Used with facing, heater plate and pressure-carrying fusion steps
- Suitable for workshop use, yard prep and site installation work
Pipe sizes, SDR ranges and job fit
Different pipe diameters call for different clamp inserts, fusion forces and heating times, so the unit is matched to the pipe set before work starts. In practice, teams use it for mainline and branch work where the pipe size sits inside the 160mm to 355mm range, the SDR call-up has been confirmed on site notes and one machine may handle several pipe wall classes across the programme.
Ovality and cut quality are checked by the operator before heating starts.
- Common use on SDR 11, SDR 13.6, SDR 17 and similar HDPE wall classes
- Works with cut pipe ends that can be faced square and clean
- Useful where different pipe batches appear on the same project
- Fits service-line work as well as longer runs laid in stages
What sits in the welding sequence
Once the bead has formed, the joint stays undisturbed during cooling so the bond can settle without twist or movement.
The machine supports that routine by keeping the pipe ends aligned while the operator works through the timing and pressure values for the pipe size in front of them. On site, weld logging helps the crew record those settings and keep the joint record tidy for handover notes or internal traceability.
- Facing for square, fresh pipe ends
- Heating with a controlled heater plate temperature
- Changeover done without dragging the joint faces
Typical jobs for the 160-355 welder
Mains, pump lines and service connections in the mid-range pipe bracket are the usual jobs for this size. Pipe runs that change size during the week, as on stormwater work, suit it as well.
Service lines, dust suppression lines and reticulation runs use this welder where the weld area must stay clean and the clamp set-up must hold firm. The machine suits sites where weather, dust and pipe handling all affect the weld face.
- Municipal water and pressure line work
- Yard-based prep before field installation
Help when the 160-355 welder reaches site
When a crew takes this machine on hire or into a new job, we set up the machine, align the clamps and check heater plate wear. Training on the 160-355mm welder teaches the fusion routine, pressure setting, bead reading and logging sheets.
Book site startup help for the first joints when the pipe programme changes by diameter or SDR. A hydraulic pressure test on this unit checks for pressure loss before the machine goes back out.
Details to confirm before the machine leaves the bay
To match the welder to the job, confirm the pipe outside diameter, SDR class, wall thickness and the longest size in the set. Clamp arrangements and support kits vary with site conditions and handling patterns.
Ask for the joint range, power setup for the hydraulic unit, heater plate condition, facer size and whether data logging needs to be built into the job file. If the order is for hire or collection, the team can also check the transport arrangement and any spare inserts needed.
- Hydraulic, heater plate and facer requirements
- Pipe size range and SDR on the drawings
Key facts
| Pipe diameter range | 160mm to 355mm |
|---|---|
| Joint method | Hydraulic butt-fusion for HDPE pipe |
| Typical pipe classes | SDR 11, SDR 13.6, SDR 17 and similar |
| Main components | Clamp set, hydraulic unit, facer, heater plate |